Wire in one door, tested assembly out the other
Six process steps and two line types, all on the same floor. Nothing is subcontracted between cutting and test — which is why a drawing revision reaches the line the same week instead of the same quarter.
- 1,500 m²
- Plant area
- 200+
- Employees
- 30,000+
- Pcs per day
- 13 yrs
- Since 2013
Eight steps, one building
-
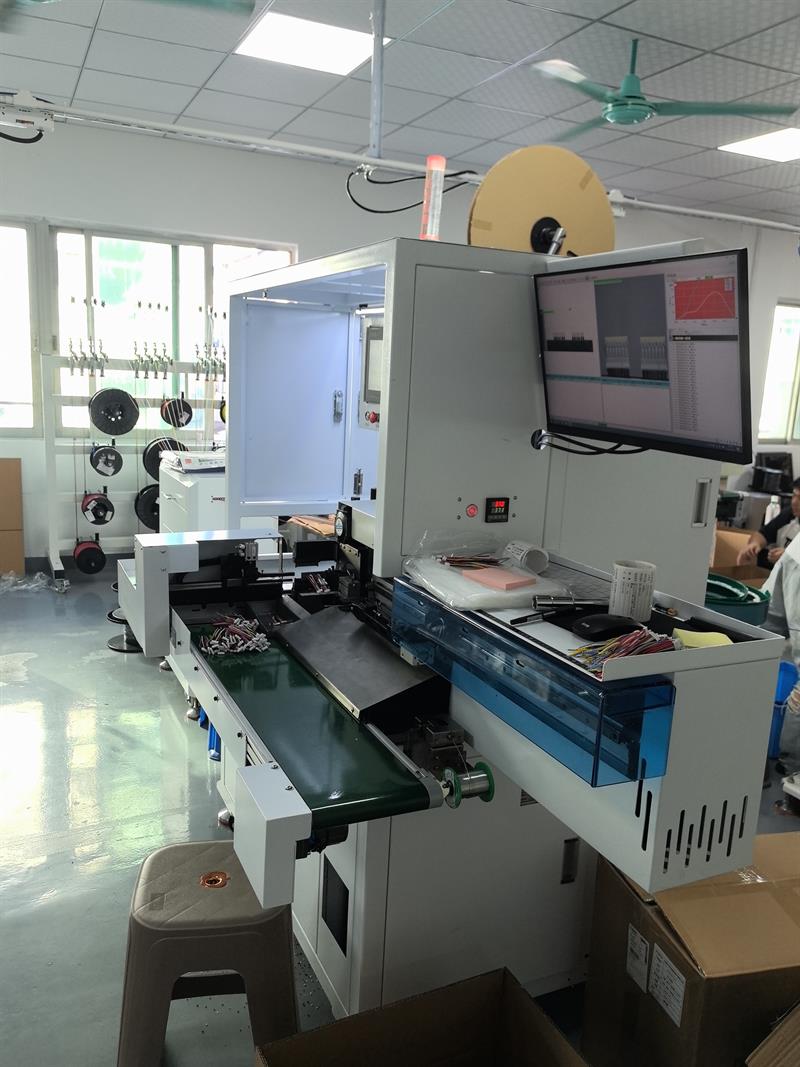 01
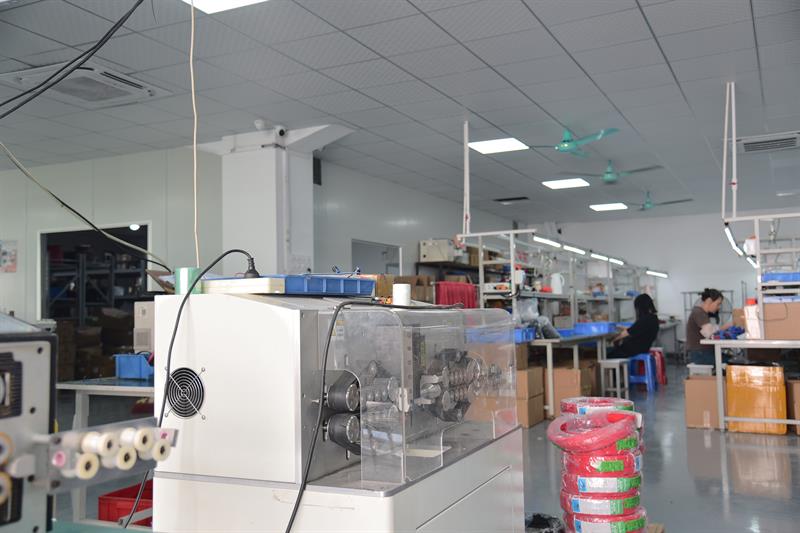
Wire cutting & stripping
Automatic cut-and-strip machines handle discrete leads from 0.5 to 6.0 mm². Cut length is held to ±1 mm; strip length to the drawing. Multi-conductor cable is processed in one pass so the cores stay in sequence.
0.5–6.0 mm² · ±1 mm cut tolerance
-
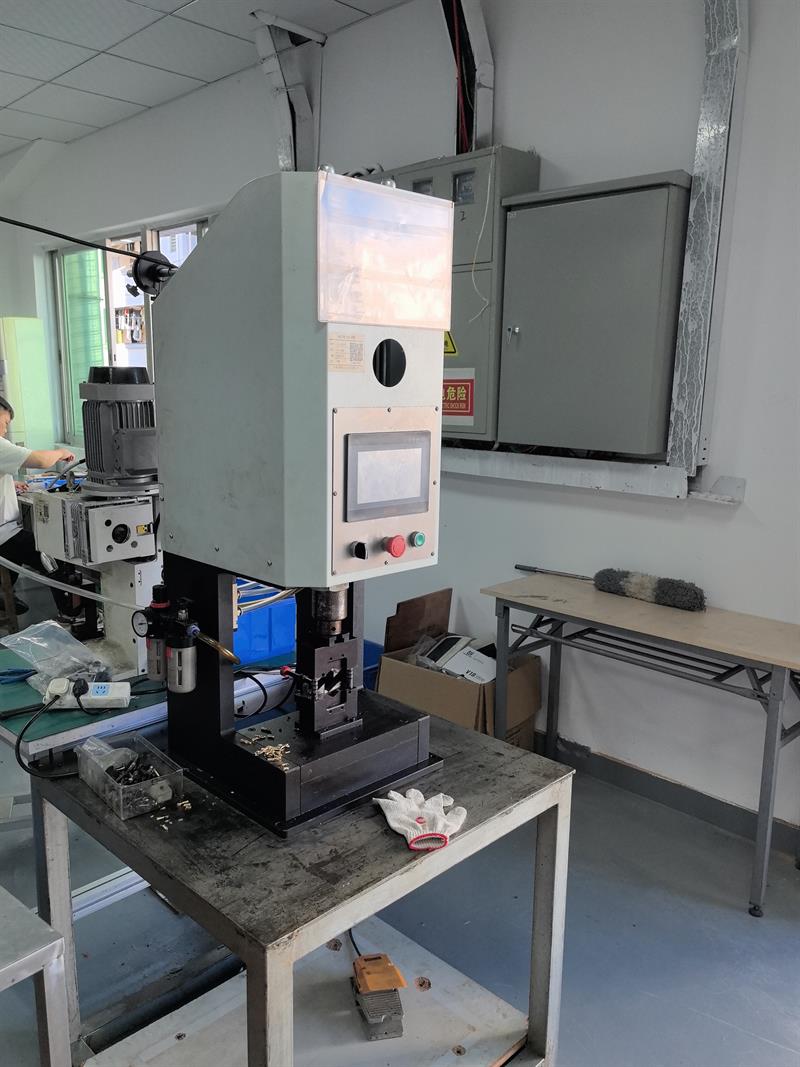 02
Crimping
Semi-automatic presses with in-line crimp-force monitoring. Crimp height is measured on a sample each batch and pull-force tested on a tension meter, with both recorded against the work order.
Crimp height + pull-force sampled per batch
-
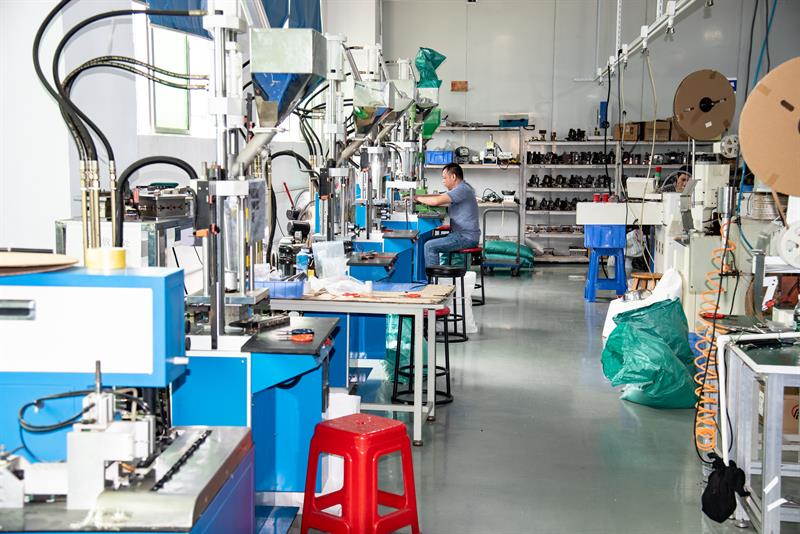 03
Injection molding
Connector bodies, strain-relief boots and small housings are molded in-house. Because the tool sits in our building, a drawing revision does not wait for a third-party molder to re-open a schedule.
In-house tooling for bodies and boots
-
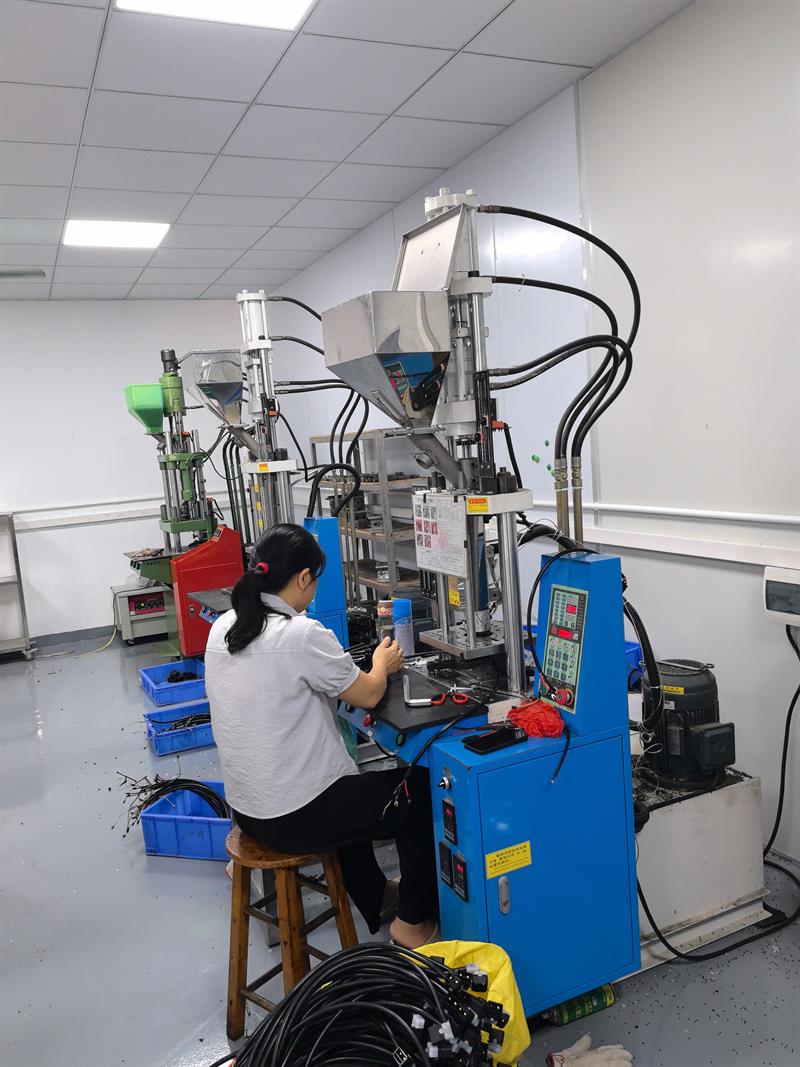 04
Overmolding
TPE and PVC overmolding for sealed cable exits and molded connector transitions. Used where the cable exit, not the connector, is the weak point — vehicle, marine and outdoor equipment.
TPE / PVC · sealed cable exits
-
 05
Assembly
Harness build on jig boards to the drawing. Branches are laid out, taped or sleeved, and the finished assembly is labelled with its part number before it moves to test.
Jig-board routing · taped or sleeved
-
 06
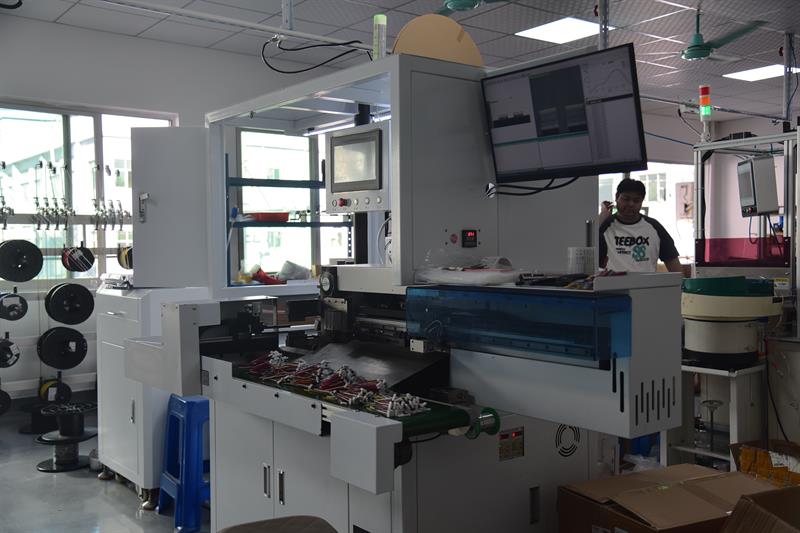
Automated production
Rotary terminal machines carry high-volume discrete leads — the single-wire and two-wire parts used in consumer products by the million. Automated lines keep unit cost and crimp consistency under control.
High-volume discrete leads
-
 07
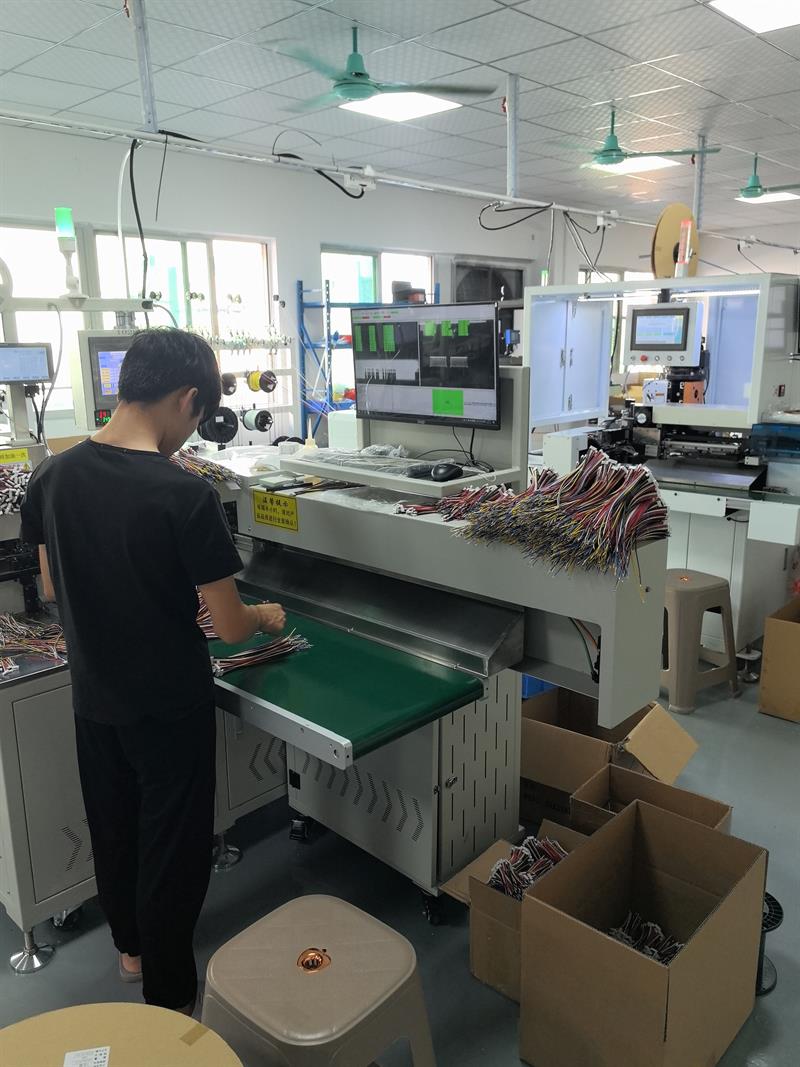
Harness line
Parallel lines for multi-branch assemblies: cut, crimp, sleeve, tape and label in sequence. Multi-branch parts are checked against the drawing at the end of the line rather than at the end of the month.
Multi-branch · sleeving · labeling
-
 08
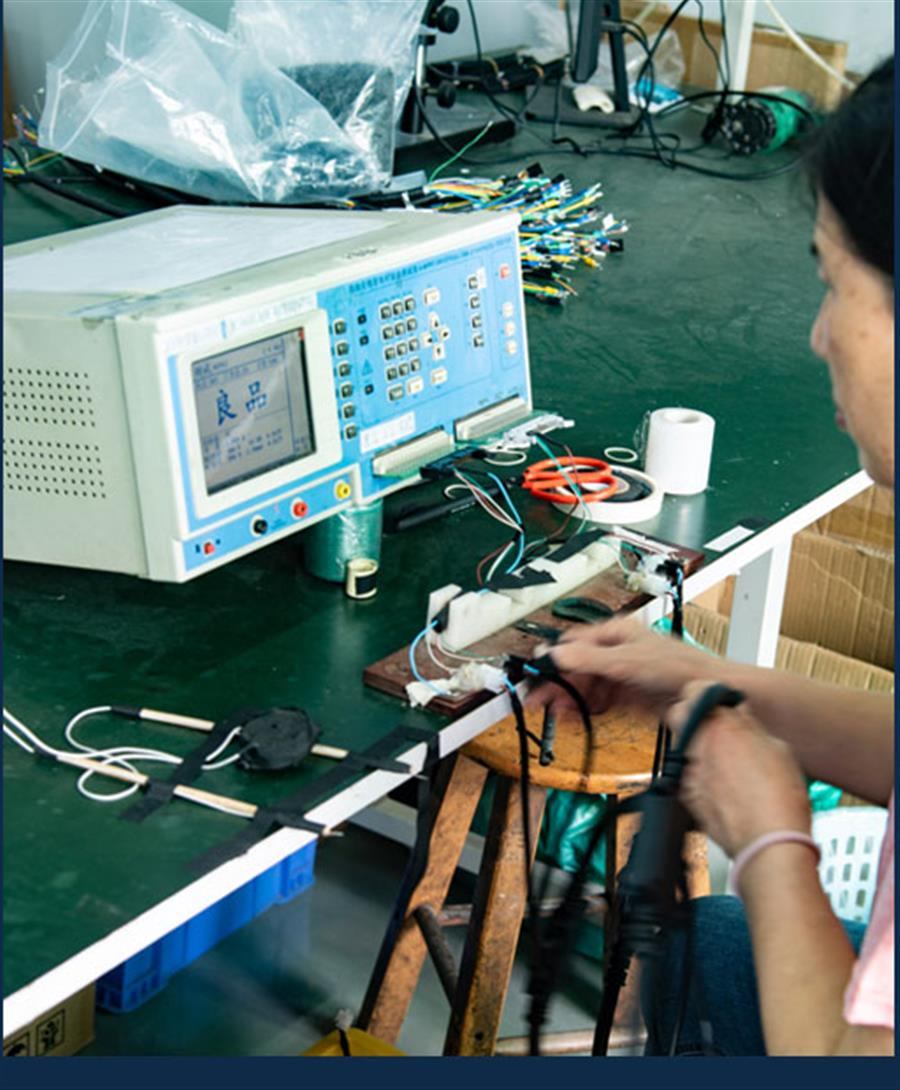
Electrical test
100% continuity on every assembly. High-current and high-voltage parts additionally get contact-resistance measurement and a dielectric withstand (hipot) test to the level on the drawing.
100% continuity · hipot on request
What we can work with
| Wire range | 0.5 – 6.0 mm² (20 – 10 AWG) discrete; heavier by arrangement |
|---|---|
| Cut length tolerance | ± 1 mm |
| Connector types | XT / EC / MR / MT / LCB, MC4, SAE, Anderson, DC barrel, M8 / M12 / M16, pluggable terminal blocks, ring and fork lugs |
| Sleeving | Heat-shrink, braided sleeve, spiral wrap, tape, conduit |
| Testing | 100% continuity; hipot and contact-resistance on request |
| Packing | Inner bag, carton, pallet; customer labeling supported |
| Daily capacity | 30,000+ pcs |
| MOQ | 500 pcs per part number (100 pcs for prototypes) |
What we need from you
- A drawing (PDF, DXF or a dimensioned sketch)
- Connector part numbers if they are specified
- Target quantity and annual volume
- Any test requirement beyond continuity
- Destination, so we can quote the shipping term
Eight areas, photographed on site
-
01 Cut & strip -
02 Crimping -
03 Injection molding -
04 Overmolding -
05 Assembly -
06 Automated lines -
07 Harness line -
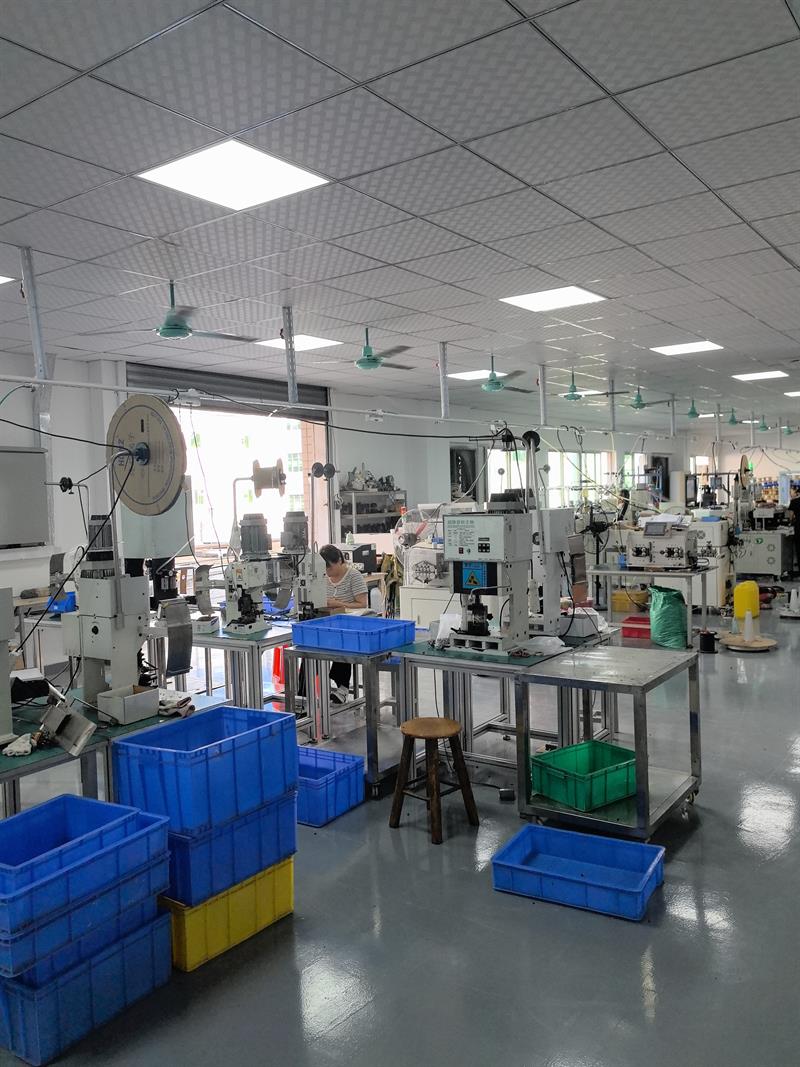
08 Production floor
Not sure whether we can build it?
Send the drawing anyway. If it is outside our range we will say so, and usually suggest who can.